본문으로 바로가기
Ess-neofab

A line- and system-level record of ESS and secondary-battery manufacturing processes

  • 한국어
  • English
  • Home
  • Process
  • System
  • Interface
  • Traceability
  • News & Trends
  • About
  • Contact
  • 한국어
  • English
  • Home
  • Process
  • System
  • Interface
  • Traceability
  • News & Trends
  • About
  • Contact

카테고리

  • Interface (28)
  • News & Trends (20)
  • Process (32)
  • System (31)
  • Traceability (22)

최근 글

  • Five million ACC cells equal 2.7 to 3.6 months of nameplate outputOctober 15, 2026
  • A 160 MW battery’s six-week commissioning has two baselinesOctober 8, 2026
  • Two Cycles a Day Take 106.8 % of a Day, and the Retention Tier Shifts Cell Volume by 1.47 GWhOctober 1, 2026
  • Battwoo’s Second-Life EV Batteries — When an 80 % Acceptance Threshold Overlaps the Retirement Distribution, Incoming Screening Becomes the BottleneckSeptember 30, 2026
  • US storage set an energy record in Q2 as installed power fell 7%September 29, 2026
  • CATL Starts Trial Production in Debrecen — The Digits of the Defect-Rate Target, Not the Equipment, Set the Length of a Trial RunSeptember 29, 2026
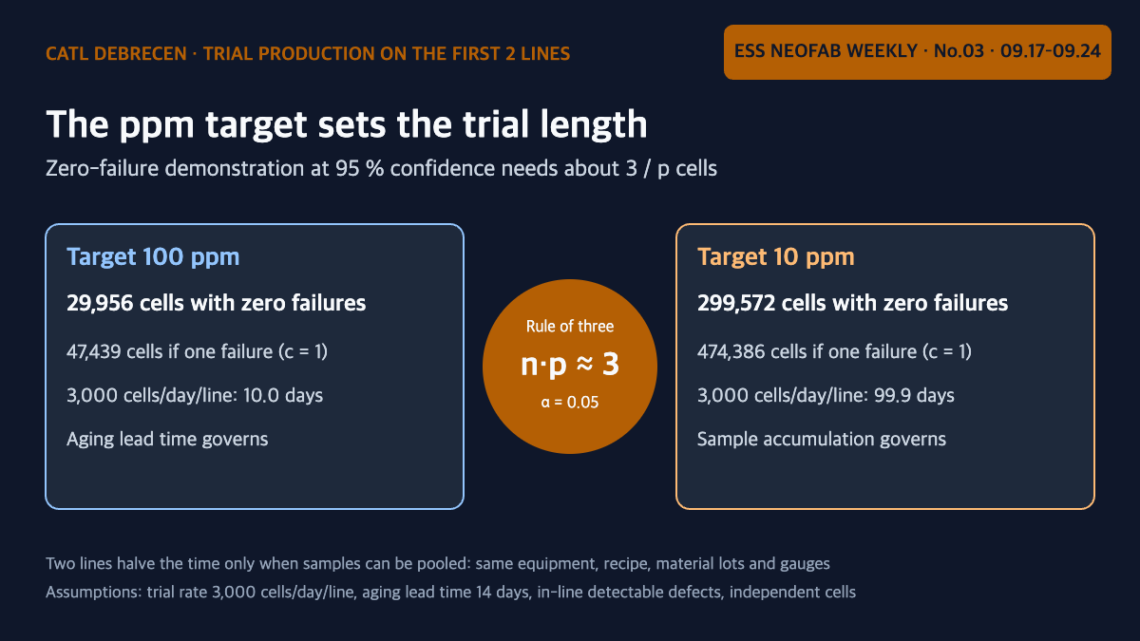
  • CATL 데브레첸 시험생산에서 목표 불량률 100 ppm과 10 ppm의 무고장 입증 표본 수와 시험생산 기간 비교 도식
    Process,  System

    CATL Starts Trial Production in Debrecen — The Digits of the Defect-Rate Target, Not the Equipment, Set the Length of a Trial Run

    September 29, 2026 /

    On September 22, 2026, CATL started trial production on the first two production lines of its cell plant in Debrecen, Hungary, stating that the purpose is "to set up, optimise and validate the production equipment and manufacturing processes ahead of series production"¹. If validation is defined as demonstrating a defect rate, a zero-failure demonstration at 95 % confidence requires 29,956 cells for 100 ppm and 299,572 cells for 10 ppm. Compared with an assumed aging-judgment lead time of 14 days, aging governs the trial length at a 100 ppm target, while sample accumulation governs it at 10 ppm. The second line halves the time only when samples are pooled, and…
    read more
    ESS-neofab 0 Comments

    You May Also Like

    Isometric concept of a line with products moving between stations at equal intervals, labeled takt time, cycle time and lead time

    Don’t Subtract Breakdowns When Calculating Takt Time — Takt Time vs. Cycle Time vs. Lead Time

    September 25, 2026
    Isometric concept of a changeover split into internal work while stopped and external work while running, from last piece to first good piece

    Is a Changeover Planned Downtime or an Availability Loss? — How the Definition Changes OEE

    September 25, 2026
    설계 능력 2.5 GWh와 셀 공급 1 GWh 조건에서 OEE가 36.9% 또는 83.8%로 보고되는 분모 분류 차이 도식

    A 2.5 GWh Line Fed Only 1 GWh of Cells — OEE of 36.9% and 83.8% Describe the Same Line

    September 25, 2026
© 2026 Ess-neofab · A line- and system-level record of ESS and secondary-battery manufacturing processes
  • About
  • Contact
  • Privacy Policy
  • Disclaimer
Ashe Theme by WP Royal.